

After twisting the carrier shaft back in July I started thinking about making new driveshafts. I have spare front and rear shafts made by Tom Woods. Over the years I've beat the snot out of them and they have held up well. However, the coating has worn off the splines and I twisted the splines on one. The buggy is never going to see street use so perfect balance is not that important. Not to mention after the first rock trail and the abuse they take they no longer would be balanced.
So, after watching a few YouTube videos I quickly became an expert on driveshaft building To simplify things, I researched driveshaft kits from a few suppliers and found exactly what I wanted. DIY 1350 2.5" tube kit with all Spicer components. I ordered two 1350 driveshaft kits and a carrier bearing kit from a reputable company (will remain unnamed). Upon unboxing the components, I thought the 1350 yokes looked a bit small but didn't pay it much mind. Fast forward a couple of weeks and I get ready to start building the shafts. First thing I notice is the 1350 yokes have a weld flange OD of 1.77". The tube is 2.5" OD .250 wall with inside of one side turned down to 2.030". I can math and yoke with a 1.77" OD does not fit inside a tube with a ID of 2.030"
 I figured someone picked the wrong yoke with boxing the stuff up. I called and explained that I think I was sent the wrong yoke. They asked me to text them pictures of the yoke.
The response "Hi Joe, I pulled one of the Spicer yokes 3-28-777 off of the shelf to verify the casting number on the yoke. The casting number is the same as yours, 3-28-239. I measured the shoulder (were the tube sits) and it measures 2.030" and the butt measures 1.77". The yoke you received is the correct yoke for the 2.0" x .250 wall tubing. The yoke will sit all of the way down into the tube for welding - picture below. "
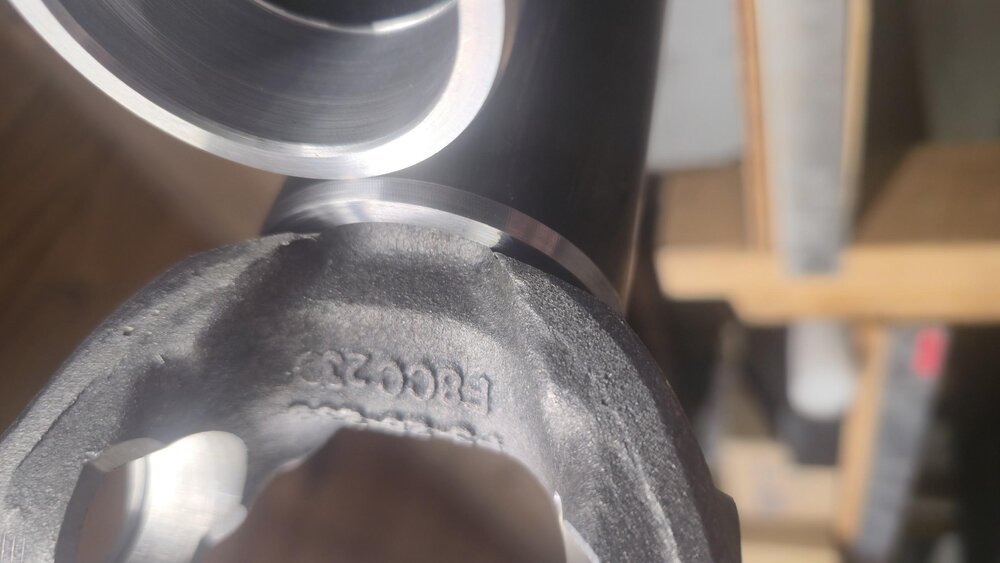
WTF That's not where the yoke is designed to be welded I looked up the Spicer part# for that yoke and it's made for a 2" .120 wall tube (doh). So I politely questioned the welding position and noted that yoke is for a 2".120 tube. I was a bit shocked at the next response: "The yoke should slide all of the way into the tube until it stops against the ears. This is the proper weld location. The 2.5" outside diameter tubing with a .250" wall thickness has the same 2" inside diameter as 2.0"x.120" wall thickness tubing. We run thicker wall tubing to provide additional strength in the driveline. The yoke that you have is the correct yoke for the 1350 DIY driveshaft kit. Thanks, ****" My response was simple "No problem, I'll throw these in the trash and order the correct yoke elsewhere".
I have never seen a yoke welded in that location and I'm fairly certain Spicer made the weld flange for a reason. I am not comfortable welding that yoke at that location and putting excessive heat into the u-joint ears. Engineers design parts a certain way for a reason. It might be fine and it might not be, but I'm not doing it!
Thoughts? Would you weld that up and trust it?
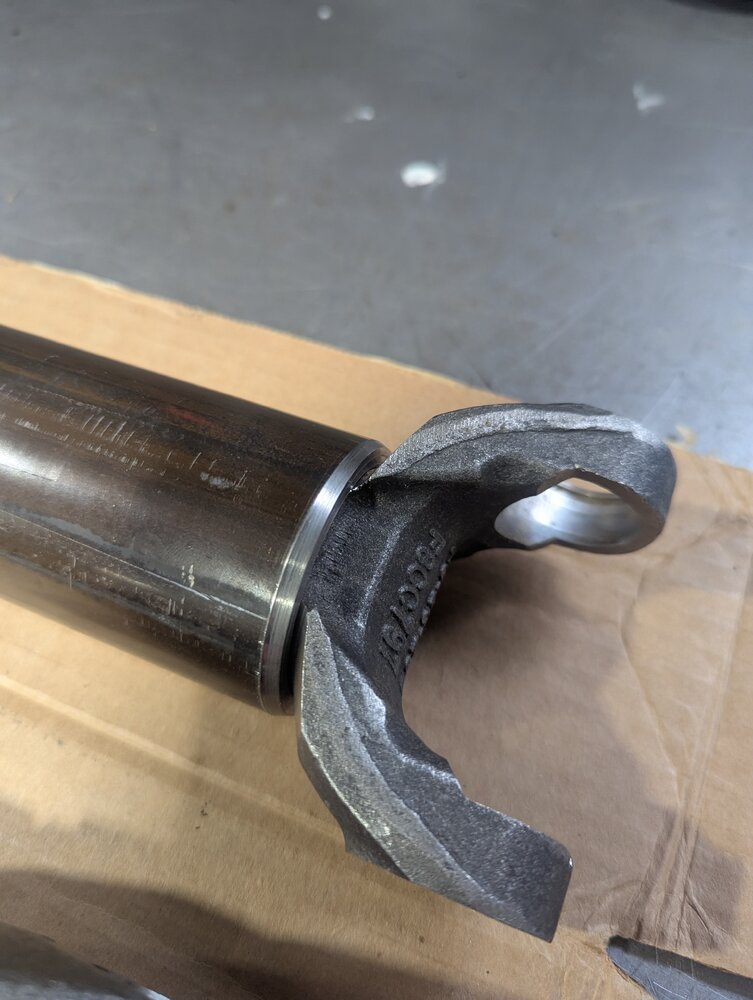
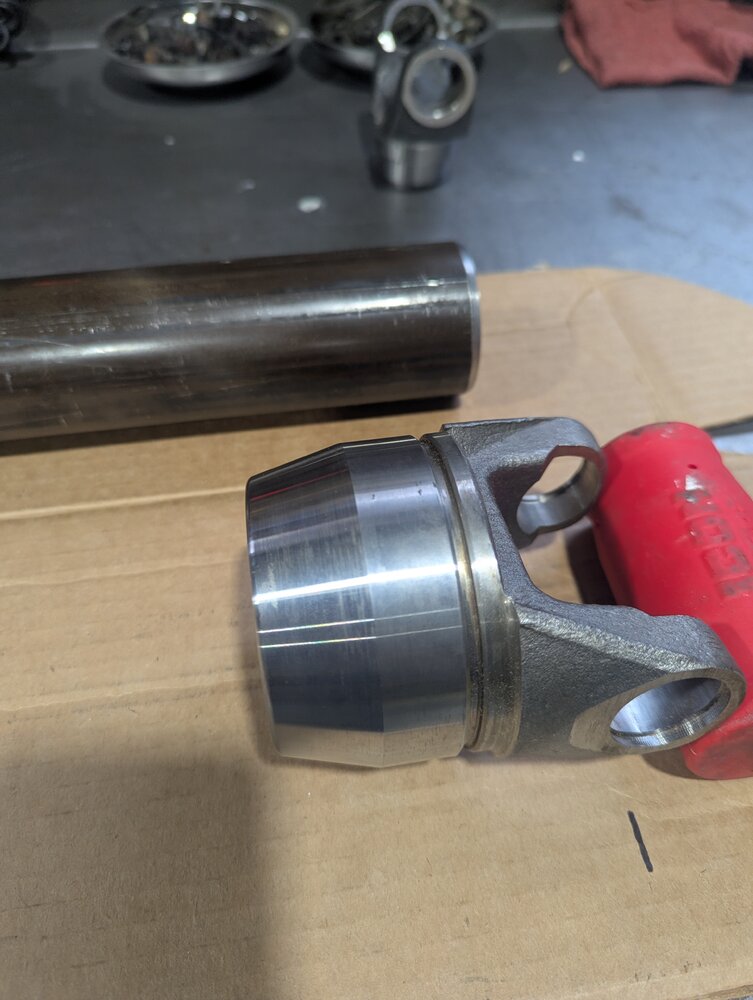
Turns out Spicer does not make a yoke for 2.5" .250" wall tubing. However, Northern Drivetrain does part# NDT-00164 but it's on national backorder and has been for some still. Work around: use a Spicer SPI-3-28-427 (3.5" .083W yoke) and a NDT-00141 (Tube yoke adapter 3.5x.083 to 2.5 ID). Ordered two of each.
Alternate yoke: Spicer 3-28-47 (2.5" .083W yoke). It has a flange of 2.345 which will require it to be turned down a bit and the tube to be opened some. Maching both the yoke and the tube should keep the thickness of both to an acceptable tolerance. Ordered and waiting on it to arrive today.
The plan it to make one of each type and determine the best solution. Last night I started making the front DS with the NDT adapter and larger #427 Spicer yoke.
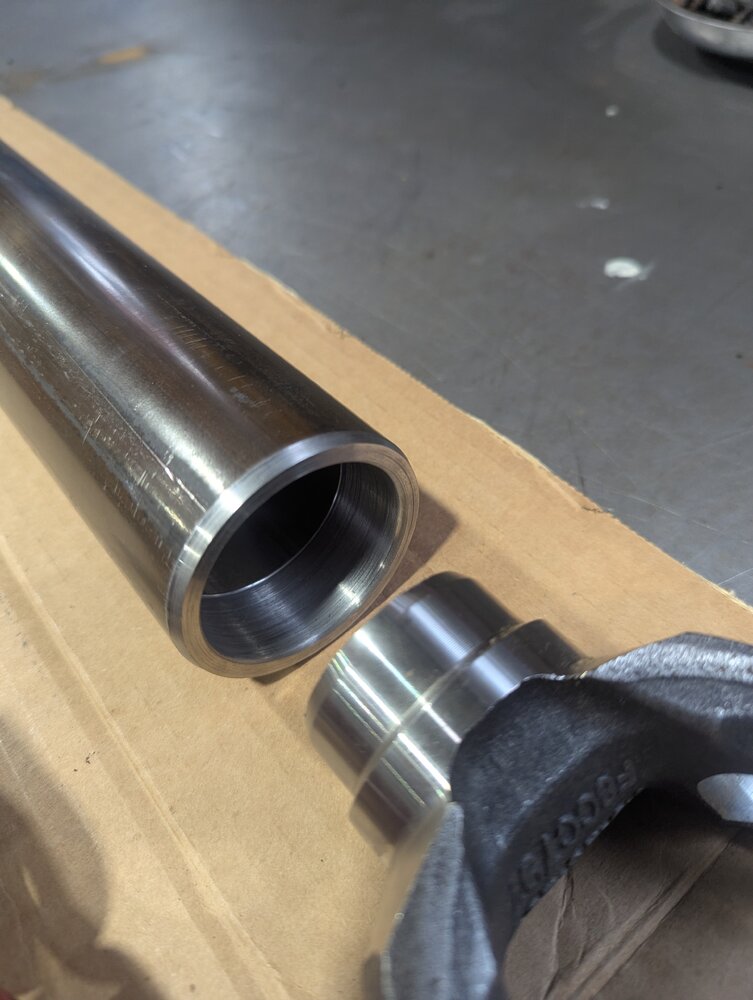
Tube cleaned up:
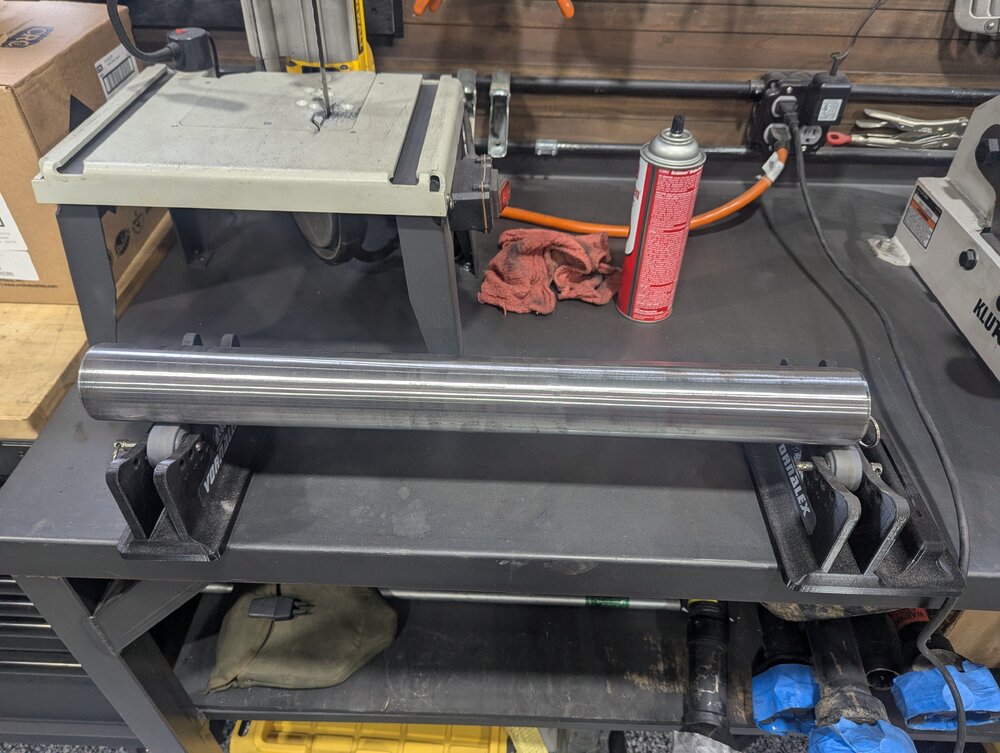
Ready to cut:
Yoke and adapter
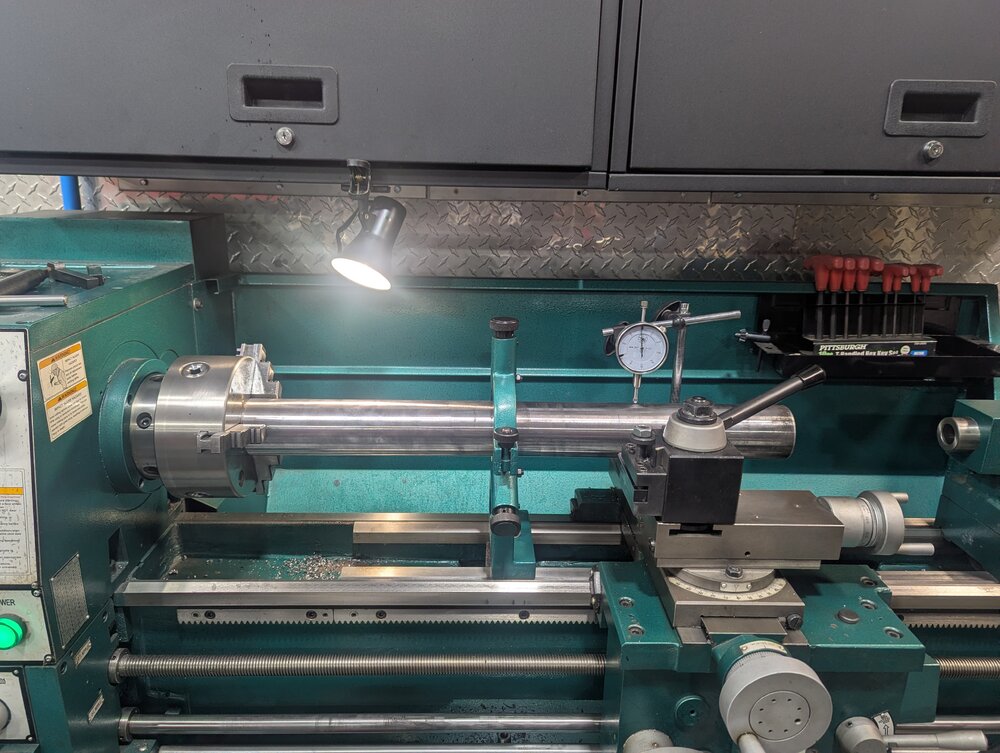
Got the tube cut to length last night and will try to get it assembled this afternoon.
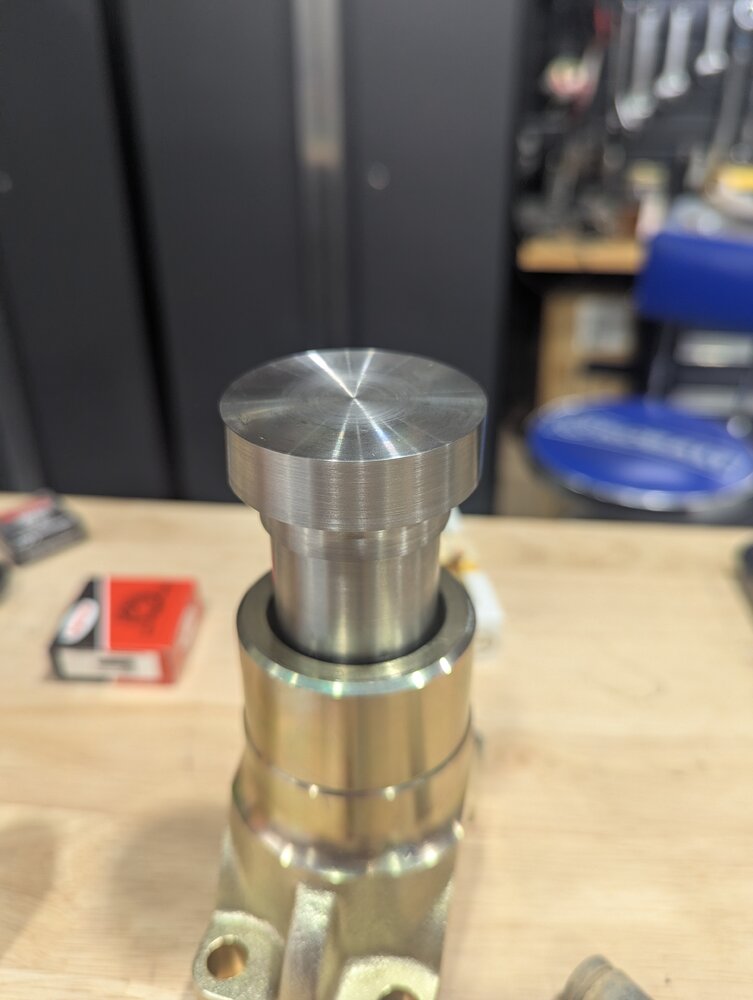
Last week I spent some time making an arbor with a live center to fit a yoke so I can try to align the DS in the lathe. We'll see how that goes
Arbor before making the live center
TBC...
So, after watching a few YouTube videos I quickly became an expert on driveshaft building
To simplify things, I researched driveshaft kits from a few suppliers and found exactly what I wanted. DIY 1350 2.5" tube kit with all Spicer components. I ordered two 1350 driveshaft kits and a carrier bearing kit from a reputable company (will remain unnamed). Upon unboxing the components, I thought the 1350 yokes looked a bit small but didn't pay it much mind. Fast forward a couple of weeks and I get ready to start building the shafts. First thing I notice is the 1350 yokes have a weld flange OD of 1.77". The tube is 2.5" OD .250 wall with inside of one side turned down to 2.030". I can math and yoke with a 1.77" OD does not fit inside a tube with a ID of 2.030" I figured someone picked the wrong yoke with boxing the stuff up. I called and explained that I think I was sent the wrong yoke. They asked me to text them pictures of the yoke.The response "Hi Joe, I pulled one of the Spicer yokes 3-28-777 off of the shelf to verify the casting number on the yoke. The casting number is the same as yours, 3-28-239. I measured the shoulder (were the tube sits) and it measures 2.030" and the butt measures 1.77". The yoke you received is the correct yoke for the 2.0" x .250 wall tubing. The yoke will sit all of the way down into the tube for welding - picture below. "
WTF That's not where the yoke is designed to be welded
I looked up the Spicer part# for that yoke and it's made for a 2" .120 wall tube (doh). So I politely questioned the welding position and noted that yoke is for a 2".120 tube. I was a bit shocked at the next response: "The yoke should slide all of the way into the tube until it stops against the ears. This is the proper weld location. The 2.5" outside diameter tubing with a .250" wall thickness has the same 2" inside diameter as 2.0"x.120" wall thickness tubing. We run thicker wall tubing to provide additional strength in the driveline. The yoke that you have is the correct yoke for the 1350 DIY driveshaft kit. Thanks, ****" My response was simple "No problem, I'll throw these in the trash and order the correct yoke elsewhere".I have never seen a yoke welded in that location and I'm fairly certain Spicer made the weld flange for a reason. I am not comfortable welding that yoke at that location and putting excessive heat into the u-joint ears. Engineers design parts a certain way for a reason. It might be fine and it might not be, but I'm not doing it!
Thoughts? Would you weld that up and trust it?
Turns out Spicer does not make a yoke for 2.5" .250" wall tubing. However, Northern Drivetrain does part# NDT-00164 but it's on national backorder and has been for some still. Work around: use a Spicer SPI-3-28-427 (3.5" .083W yoke) and a NDT-00141 (Tube yoke adapter 3.5x.083 to 2.5 ID). Ordered two of each.
Alternate yoke: Spicer 3-28-47 (2.5" .083W yoke). It has a flange of 2.345 which will require it to be turned down a bit and the tube to be opened some. Maching both the yoke and the tube should keep the thickness of both to an acceptable tolerance. Ordered and waiting on it to arrive today.
The plan it to make one of each type and determine the best solution. Last night I started making the front DS with the NDT adapter and larger #427 Spicer yoke.
Tube cleaned up:
Ready to cut:
Yoke and adapter
Got the tube cut to length last night and will try to get it assembled this afternoon.
Last week I spent some time making an arbor with a live center to fit a yoke so I can try to align the DS in the lathe. We'll see how that goes
Arbor before making the live center
TBC...


